OEM Abrasive Jumbo Roll Solutions for Efficient Surface Finishing
2026-09-20
Surface finishing shouldn't be a bottleneck. For manufacturers who demand consistent results on every pass, OEM abrasive jumbo rolls offer a smarter path—and SHENZHEN SUN ABRASIVES is quietly redefining what 'efficient' really means.
How Custom Jumbo Rolls Cut Changeover Time Without Sacrificing Finish Quality
Swapping a standard jumbo roll mid-run usually means stopping the line, wrestling with alignment, and then spending precious minutes dialing tension back in. That downtime isn't just lost output; it often leads to uneven coating or visible wrap lines once the machine restarts. Custom jumbo rolls flip that equation. By matching the core diameter, width, and material gauge to the exact unwind stand, the new roll seats correctly the first time. Operators can make the switch in a fraction of the time—often without touching a single tension setting because the incoming roll behaves the same as the outgoing one.
Finish quality doesn't get sacrificed for speed because the custom roll is built around your specific process parameters. Instead of forcing a generic roll to fit, the converter adjusts things like surface roughness, edge trim, and static dissipation to match what your coating or laminating line already expects. That means the fresh roll runs with the same web stability, the same draw characteristics, and the same lay-flat behavior as the previous roll. The result? Fewer micro-stretches, no sudden tension spikes, and a seamless handoff that leaves no visual witness marks on the finished product.
What really sets custom jumbo rolls apart is how they smooth out the human factor. When operators know the next roll is a drop-in replacement, they don't rush the splice or guess at brake pressure. Inventory can be scheduled with longer uninterrupted runs, and changeovers become routine rather than a source of quality risk. Over time, this predictable changeover rhythm reduces scrap at the start of each new roll and keeps your finish quality consistent from the first meter to the last.
A Practical Way to Match Grain Structure to Substrate for Consistent Results
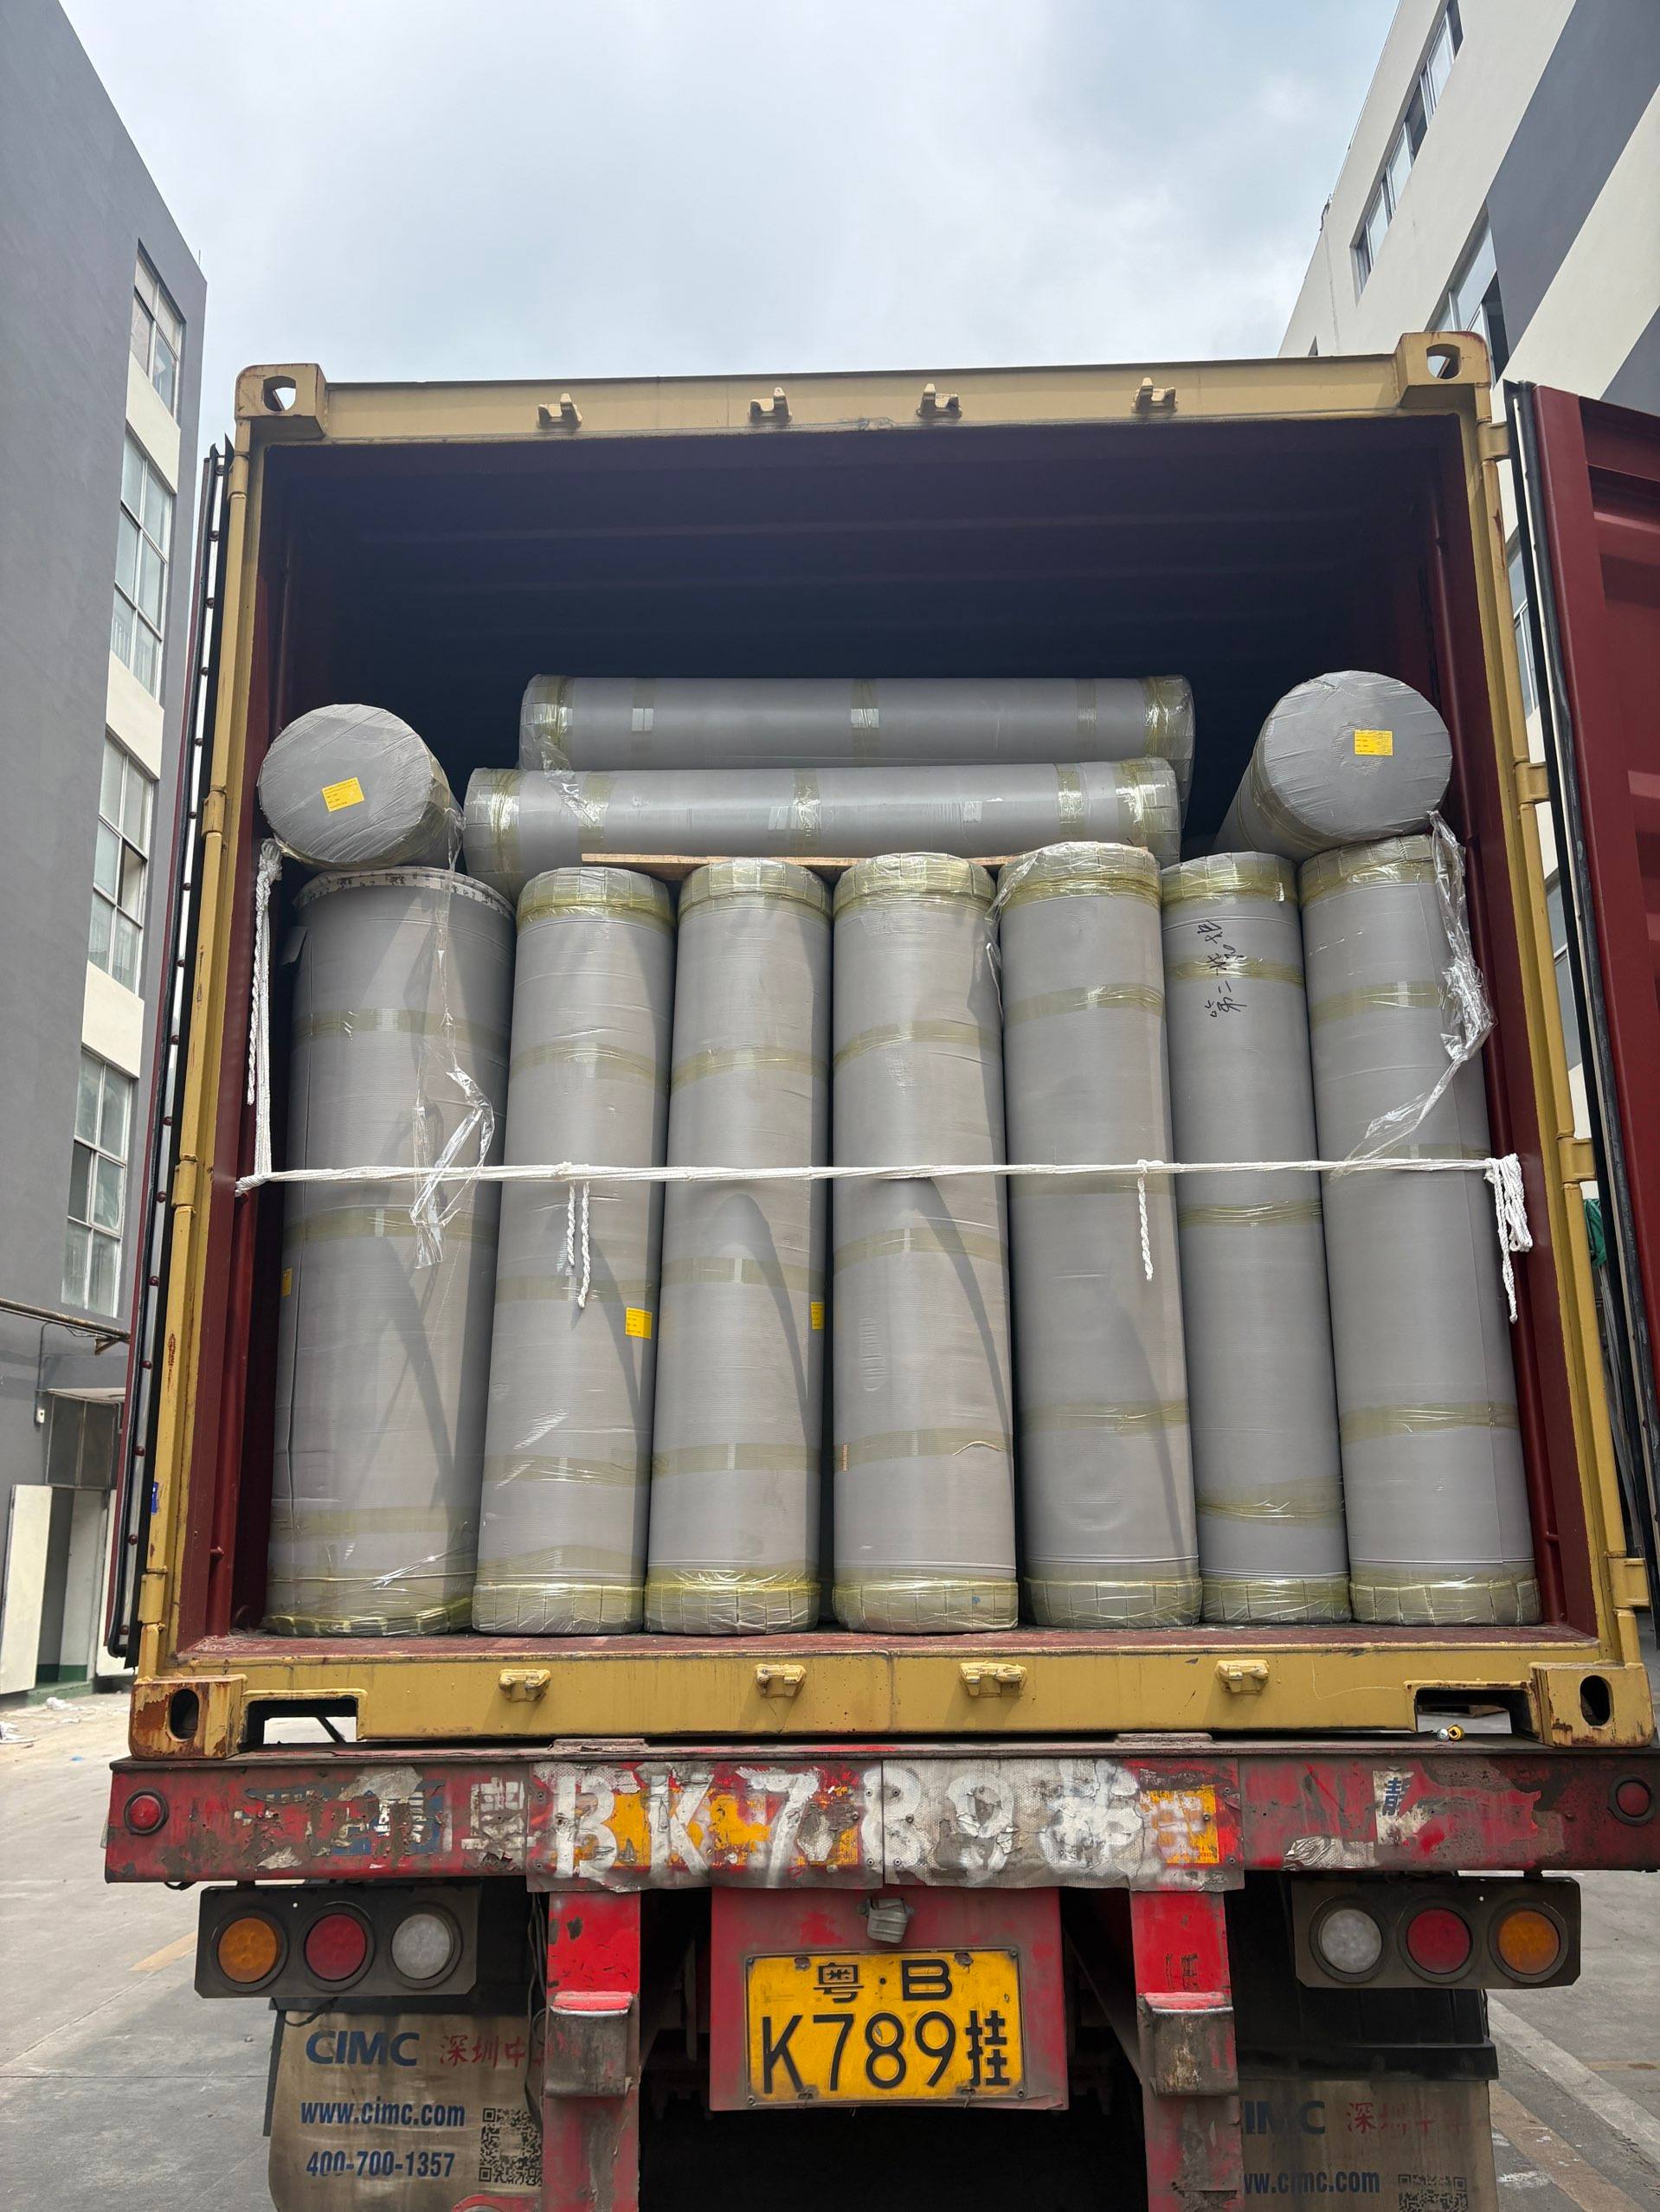
Start by making a quick study of the substrate under low-angle light. Run your fingers across it and note whether the grain runs in one direction, changes near edges, or has shallow chatter marks. On a separate test piece, use the same abrasive sequence you plan to use on the workpiece. Begin one grit coarser than your first guess, then move to finer grits only until the scratch pattern disappears into the substrate’s existing texture. This usually gets you closer than trying to copy the grain from a photo or memory.
Once the direction and depth feel close, blend a small area and let it dry or cure fully before judging. The grain often looks finer when wet or coated, so an early check can mislead you. If the test patch stands out, resist the urge to polish the whole surface. Instead, change one variable at a time—lower the pressure, shorten the stroke, or rotate the final pass by a few degrees—and compare the edge of the patch under the same lighting. The goal is a transition you can’t locate by eye.
To keep results repeatable, treat your setup like a simple recipe. Note the abrasive type, backing pad, speed, and number of passes for that specific substrate. Store the test piece with the recipe, not just the finished part. When you return to the same job weeks later, that reference sample saves more time than any written description. Over time you’ll build a small library of matched samples that makes the next project start closer to the mark.
The Hidden Costs of Standard Roll Widths in High-Volume Finishing
Standard roll widths look like a safe choice until you trace what happens across a month of high-volume runs. A finishing line set up for 60-inch stock may handle a 54-inch job, but the leftover six-inch strip rarely finds another use. Multiply that by dozens of orders and the offcuts turn into a steady stream of trim waste, extra handling, and disposal fees that never appear on the initial material quote.
The less visible cost sits in changeover time. When standard widths force operators to shim, adjust guides, or run multiple narrow rolls side by side, each switch eats into productive hours. Over three shifts, those minutes compound into lost capacity that could have run additional jobs. Floor space also suffers because you end up storing several standard widths instead of one optimized size, tying up inventory dollars and creating more forklift traffic.
There is also a quality angle that gets overlooked. Running material under tension at a width that does not match the job can cause tracking drift, wrinkles, or registration shifts, especially on long runs. The resulting rework or rejected output quietly erodes the margin you thought you saved by buying standard stock. In high-volume finishing, the real cost of a roll is not its price per pound but how much of it actually becomes sellable product.
Fine-Tuning Abrasive Flexibility for Contoured and Hard-to-Reach Surfaces
Getting abrasives to follow a compound curve or slip into a tight corner usually means trading away either cut rate or edge life. The fix rarely comes from changing grit alone; it comes from rethinking the backing and the bond so the abrasive can flex without bunching or tearing at the edges. Thin film backings with a controlled stretch, paired with a bond that releases spent grain gradually, let the disc wrap around a radius while still keeping enough pressure on the high spots to remove material evenly.
For narrow gaps and recessed areas, the shape of the tool matters as much as the abrasive itself. Tapered points, flap wheels with angled packs, and low-profile disc holders reduce the amount of tilting needed to reach the work surface. That keeps the abrasive face flatter against the contour, so wear spreads across more of the grain instead of concentrating at a single fold line. The result is a more consistent scratch pattern and fewer hand-touch passes after the machine work is done.
On deep contours where standard discs chatter or skip, reducing the abrasive's inherent stiffness at the center while keeping the outer edge slightly firmer helps the tool settle into the profile. This can be done by varying the coating weight, using a segmented or slotted backing, or switching to a non-woven blend that crushes to match the shape. Operators often find that a combination of a softer interface pad and a thinner abrasive film removes the need to switch between multiple tools on the same part, cutting down the time lost to chatter marks and rework.
Signs Your Finishing Line Is Ready for a Custom Roll Specification
If you're constantly chasing the same streak or chatter mark across the web, that's usually the first clue. Standard rolls ship with generic hardness and finish profiles, which work fine until a line settles into its own rhythm of speed, tension, and coating weight. When operators start shimming, adjusting pressure, or swapping rolls mid-shift just to keep edges clean, the mismatch has already moved from annoyance to real downtime.
Changes in what you're actually running through the line matter just as much. A shift to thinner substrates, higher-solids coatings, or faster drying cycles changes how the roll surface needs to grip and release. If the existing roll diameter or surface texture was picked for an older product mix, you'll see it in uneven laydown, more wrap-ups, or a finish that looks good on one side and thin on the other.
Another sign is the maintenance log. When roll regrinds become more frequent, or a roll that used to last a full season now needs attention every few weeks, that's not just wear—it's the line telling you the specification has drifted out of range. A custom roll matched to your actual speeds, chemistries, and defect patterns often pays for itself by cutting scrap and giving operators back the hours they used to spend correcting a stock-spec compromise.
Balancing Aggressive Stock Removal with a Uniform Final Surface
Stripping away material fast usually leaves a rough, uneven landscape that demands extra passes to clean up. The trick is knowing when to back off the feed rate and let the tool's geometry do the finishing work. A coarse step-over might chew through stock in minutes, but the ridges it leaves behind can sabotage any hope of a consistent surface. Switching to a smaller radial engagement near the end of the roughing cycle lets the same cutter knock down the peaks without a tool change, saving setup time while keeping the final topography within spec.
Many machinists treat aggressive removal and fine finishing as separate worlds, but the real skill lies in blending them. By ramping down the depth of cut incrementally instead of jumping straight to a finish pass, you avoid shocking the tool and the part. Thermal buildup from heavy cuts warps thin sections, so easing off gradually lets the workpiece settle back to its true shape before the last light skim. That middle ground produces a surface that looks uniform to the eye and measures consistently under a profilometer.
Tool path strategy also plays a quiet but critical role. Climb milling with a slight overlap on each pass prevents the step marks that plague conventional roughing. And if the spindle speed stays constant while the feed drops, the chip thickness thins out, which actually improves the shearing action rather than rubbing the surface. The result is a part that comes off the machine with a near-finished face, ready for anodizing or light deburring instead of a lengthy secondary operation.
FAQ
They are manufactured to match specific equipment and process requirements, so width, splice pattern, backing weight, and grain type are all tailored rather than forcing your line to adapt to a generic product.
Fewer roll changes and less downtime because the jumbo format reduces splice frequency. Consistent abrasive exposure also means fewer passes to hit the required finish, which speeds up throughput.
Metal fabrication, woodworking, automotive body shops, and composite manufacturing tend to see the biggest gains, especially where wide belt or long stroke sanding is part of daily production.
Yes. Aluminum oxide, zirconia, ceramic, and silicon carbide can be specified, along with open or closed coat, grain size, and bonding resin, so the roll performs well on everything from soft wood to hardened steel.
Polyester, cotton blends, and film backings are all available in different weights. For high-pressure grinding or deburring, a heavier X-weight or Y-weight cloth usually resists tearing and extends roll life.
Because the roll width and length are matched to your converting equipment, you're not trimming off as much unused edge material. Longer runs also mean fewer stub rolls left at the end of a production batch.
Confirm the exact grain type, bond system, backing flexibility, roll diameter limit on your unwind stand, and whether you need a specific splice configuration for your machine.
It depends on the bond and backing. Waterproof paper or polyester backings with resin over resin bonds handle wet applications well, while traditional cloth rolls are usually better for dry grinding.
Conclusion
Switching to OEM abrasive jumbo rolls often starts as a way to cut changeover time, but the real payoff comes from how that change ripples through the whole finishing line. Instead of stopping production to swap narrow rolls every few hours, a properly specified jumbo roll keeps the line moving longer. What surprises many shops is that finish quality does not have to take a hit. The key is pairing the roll's grain structure to the substrate—whether it is aluminum, stainless steel, or a coated surface—so the abrasive cuts consistently instead of loading up or leaving random scratches. The hidden costs of standard roll widths are easy to overlook until you track downtime and waste. Off-the-shelf widths force operators to either run multiple narrow strips or trim wide rolls down, both of which create scrap, splice points, and uneven tension. A custom jumbo roll sized to your exact line width eliminates those seams and keeps the abrasive surface uniform across the entire workpiece.
Contoured and hard-to-reach areas demand more than a one-size-fits-all abrasive. With a custom jumbo roll, you can fine-tune flexibility, backing weight, and grain type so the abrasive conforms to curves without tearing or skipping. That matters when a single pass needs to remove stock aggressively yet leave a consistent final surface. Too stiff and you gouge edges; too soft and you lose cutting power. A well-specified roll balances those forces by adjusting grain size, bond type, and open-coat structure. So how do you know your finishing line is ready for a custom specification? Watch for frequent roll changes, rising scrap rates from splice marks, inconsistent scratch patterns, or operators struggling to reach recessed areas. When standard rolls force compromises between speed, finish, and downtime, a custom OEM jumbo roll becomes less of an upgrade and more of a necessity for efficient surface finishing.
Contact Us
Contact Person: Amanda Wang
Email: [email protected]
Tel/WhatsApp: +86-13602569854
Website: https://www.sunabrasives.com.cn