Top Ultrasonic Coating System: Key Features to Look For
2026-09-20
Choosing the right ultrasonic coating system can make or break your precision coating process—especially when uniformity, repeatability, and material efficiency are non-negotiable. But with dozens of options on the market, how do you separate a truly capable system from one that just looks good on paper? In this guide, we break down the key features that actually matter, from nozzle design and flow control to software integration and long-term reliability. Whether you're coating medical devices, electronics, or advanced materials, Siansonic has been at the forefront of ultrasonic coating innovation, and these are the specs you should insist on before making your next investment.
Nozzle Stability That Survives Back-to-Back Shifts
Most nozzles behave fine for the first hour. It’s the third handoff, after the housing has heated and cooled twice, that tells you what the design is actually worth. The locking collar on this one doesn’t rely on a single stiff thread; it uses a stepped shoulder that settles into the seat and stays put even when someone cranks the line pressure at 2 a.m.
What usually kills stability across shifts isn’t impact—it’s the slow loosening caused by thermal cycling. Hot fluid expands the seat, cold rinse shrinks it, and the nozzle starts backing off in tiny increments. Here the retainer ring and the body are cut from the same alloy, so they grow and shrink together instead of fighting each other. That means the spray angle stays narrow and the fan stays even, hour after hour.
After two weeks of running three shifts, maintenance noticed the adjustment screws hadn’t moved from their initial marks. No one had to retorque the collar during changeover, and the pattern check at the start of each shift was basically a formality. That’s the kind of stability you stop thinking about—and that’s the point.
Predictable Coating Thickness Across Large Panels
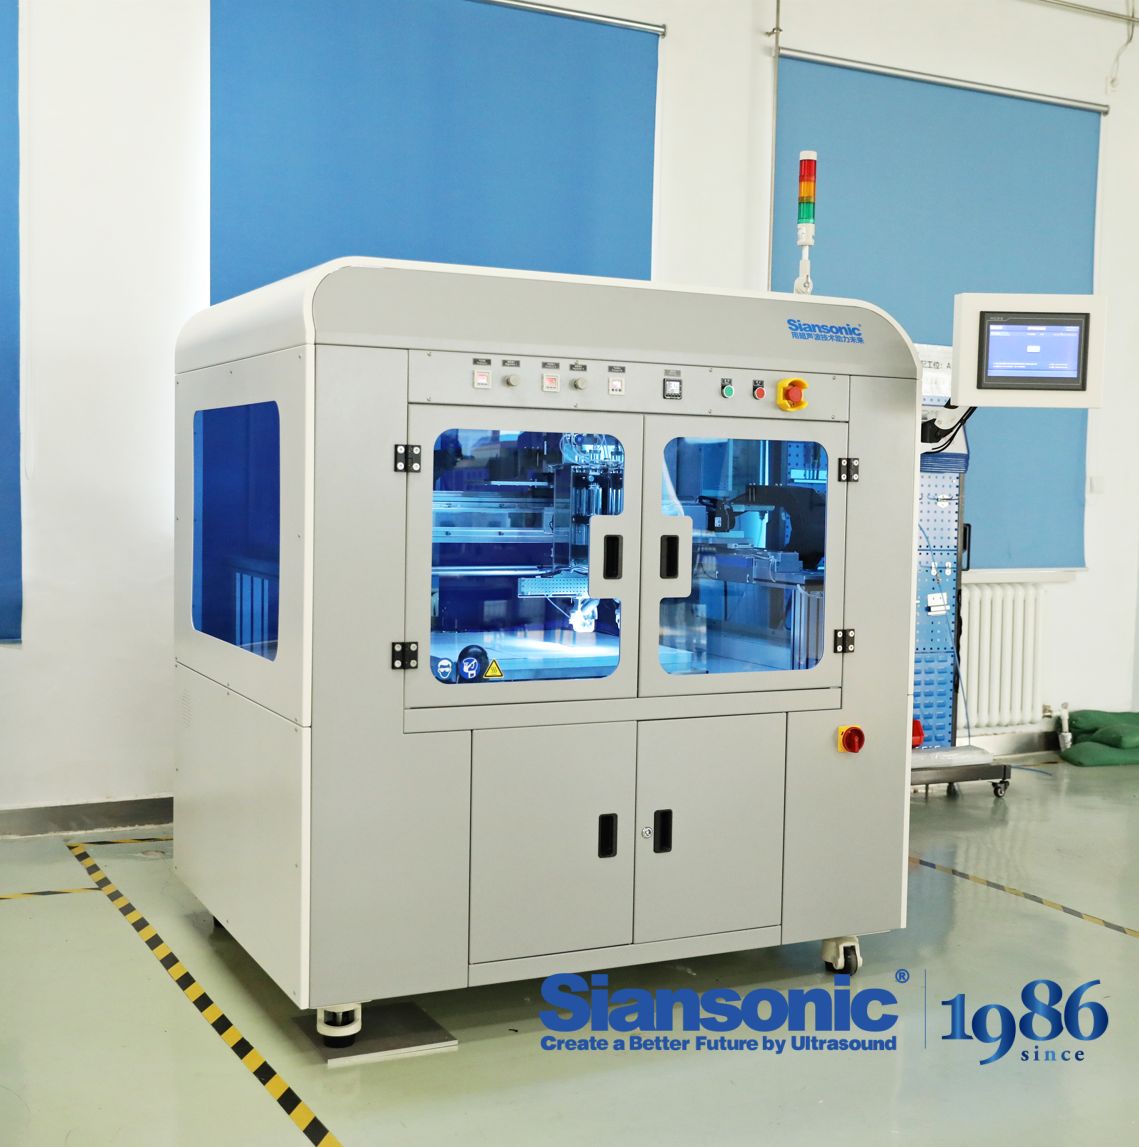
Achieving consistent film build on oversized substrates rarely comes down to a single setting. Operators often learn that nozzle distance, traverse speed, and fluid pressure interact in ways that static charts can't capture. On a four-meter panel, a two-second dwell variation near the edges can shift dry film thickness by several microns, which later shows up as visible banding under gloss inspection.
The move toward closed-loop thickness monitoring has changed how shops approach large-format work. Instead of relying on periodic wet-film gauges, inline sensors now track deposit patterns across the full width and feed adjustments back to the spray controller. This keeps the center-to-edge deviation within a narrow band, even when ambient temperature or coating viscosity drifts through a shift.
For panels that will be edge-banded or joined, predictable thickness also means fewer surprises at assembly. A panel that measures within tolerance in the middle but falls off near the corners can create a step at the seam or require extra sanding. By mapping the spray pattern over several runs, coaters can build a reference profile for each substrate size and lock in parameters that repeat from batch to batch.
Real-Time Flow Tweaks Without Halting the Run
Traditional batch jobs expect you to commit to a set of parameters before the first record is processed. But modern orchestration layers let you slide a gain factor, switch sampling rates, or even reroute a branch while the pipeline is still chewing through data. The trick is to keep the runtime state in a shared, versioned store rather than baking it into the job’s local memory. When a tweak arrives, each worker picks it up at the next checkpoint instead of restarting from zero.
We’ve seen teams use this to nudge a stream processor’s watermark threshold mid-run because a sensor network started drifting. No downtime, no lost offsets. The key is to make the control signals idempotent and to log every adjustment with the same rigor as the data itself. That way, if a downstream model starts misbehaving, you can bisect exactly which tweak caused the shift—not just guess.
Another practical pattern is to expose a tiny sidecar API that accepts partial config deltas. The main loop never blocks; it just consults the delta on a fixed cadence. This turns 'stop and redeploy' into 'adjust and observe.' The result is a system that feels less like a fragile batch script and more like tuning a guitar while it’s still being played.
Substrate Flexibility That Skips the Tooling Overhaul
Traditional workflows treat substrate changes as a trigger for re-tooling. Swapping from one material to another often means replacing fixtures, recalibrating grippers, or adjusting vacuum patterns. The idea behind substrate flexibility is to make the substrate itself carry the adaptation logic, so the existing equipment keeps working without mechanical changes. A surface with locally tuned stiffness or embedded alignment features can settle into place using the same force and path as before, even if the base material is different.
In flexible circuit production, moving from rigid glass panels to polyimide films usually forces a line stop for vacuum chuck reconfiguration and optical target re-teaching. That step disappears when the substrate is designed to match the tool’s existing constraints. For example, adding microscopic ridges along the edges of a thin film can mimic the handling behavior of a thicker board, letting the same end effector pick it up without slip or sag. The tool never knows the difference.
The real payoff is not just saved minutes. Avoiding tooling overhauls means no risk of introducing alignment drift or wearing down quick-change interfaces. It also allows mixed substrate batches on one line, which is rare in conventional setups. For low-volume, high-mix manufacturing, this flexibility turns a costly bottleneck into a non-event.
Maintenance Alerts That Arrive Before the Fault
Most maintenance systems wait until something breaks. By then, the damage is done: production halts, repair costs spike, and everyone scrambles. Our approach flips that timeline. Sensors and machine learning work quietly in the background, learning the normal rhythm of every motor, pump, and conveyor. When the vibration pattern shifts a fraction of a millimeter from baseline, or a bearing temperature climbs three degrees above its usual range, the system doesn't just record it—it sends an alert. Not a vague warning about 'potential issues,' but a specific nudge: check the third drive belt on Line 2, expect wear within the next two weeks.
What makes these alerts useful is their timing. They arrive early enough to schedule a fix during planned downtime, not late enough to trigger an emergency call at 3 a.m. Maintenance crews stop chasing ghosts and start following a prioritized list. One plant manager described it as finally seeing the potholes before the axle snaps. The alerts don't cry wolf either—each one is tied to a measured deviation, with a confidence score that separates genuine anomalies from normal operational noise.
The result is a quieter factory floor, fewer unexpected stops, and parts that get replaced on their own terms. Technicians spend less time reacting and more time improving. The system never sleeps, never gets distracted, and never assumes 'that noise has always been there.' Instead, it keeps a continuous, honest record of what healthy looks like—and tells you the moment health starts to fade.
Process Data You Can Actually Act On Mid-Batch
Waiting until the end of a production cycle to check data means you're stuck reacting to problems you could have prevented hours ago. Mid-batch processing flips that timeline: pull in temperature readings, humidity levels, or torque values as they're generated, flag deviations right then, and let operators adjust before the next unit gets built.
The trick is keeping the analysis simple enough to run on the line. You don't need a full analytics suite; a small set of rules built around your specific tolerances catches most issues. When a reading drifts outside the expected band, the system can send a direct alert to the line lead's tablet, showing exactly which sensor, what value, and how long it has been off.
That kind of immediacy changes the conversation from "what happened on yesterday's shift" to "let's fix this before lunch." It also means the data you collect actually earns its keep, instead of sitting in a report nobody opens until the monthly review.
FAQ
Start with the nozzle's operating frequency and the generator's power range. A system running at 20 kHz handles thicker, higher-viscosity fluids better, while 60 kHz or 120 kHz gives finer atomization for very thin, precise layers. Also confirm the maximum flow rate matches your production speed, not just your lab trials.
Yes, frequency directly affects droplet size and spray pattern. Lower frequencies produce larger droplets with more kinetic energy, which can be useful for penetrating textured surfaces. Higher frequencies create a softer, narrower spray with droplets under 10 microns—ideal for delicate substrates like medical stents or thin-film electronics.
They can, but you need to check the nozzle material and feed path design. Look for titanium or ceramic nozzle tips rather than stainless steel, and ask about replaceable wear components. A system with an easy-access liquid line and no fine mesh filters will save you hours of downtime when using ceramic-filled or metallic-pigment coatings.
Closed-loop flow control combined with a precise motion platform is the key. If the system only controls ultrasonic power but not the liquid delivery rate, you'll see thickness drift as tank level or viscosity changes. Demand a system that monitors both flow rate and frequency in real time, and ask to see uniformity data across a 300 mm or larger substrate, not just a 50 mm coupon.
In most high-yield settings, yes. Closed-loop feedback adjusts pump speed or ultrasonic amplitude within milliseconds to compensate for temperature shifts, viscosity changes, or line speed variations. Without it, an operator has to manually dial in corrections after every batch, which leads to lot-to-lot inconsistency that customers will notice.
Look for a system that supports gentle heating of the fluid reservoir and a low-pulsation pump, like a syringe or peristaltic design, rather than a gear pump. An ultrasonic nozzle with a built-in flushing port or a quick-disconnect tip also makes clean-up far less painful. The goal is to keep the fluid moving smoothly without overheating or shearing it.
It plays a bigger role than most people expect. Flexible films, porous ceramics, and three-dimensional parts each need a different spray distance and atomization energy. If you are coating temperature-sensitive polymers, you'll want a system with very low air pressure or an entirely airless design to avoid cooling or deforming the surface. Always test on your actual substrate, not a glass slide.
Ask if the vendor offers free sample coating trials with your own fluid and substrate, and how quickly they can ship replacement nozzles. A strong partner will provide detailed setup documentation, training on resonance tuning, and a clear answer on mean time to repair. Avoid vendors who only sell the hardware and disappear after installation.
Conclusion
A top ultrasonic coating system earns its place on the factory floor by staying dependable when demand peaks. The nozzle assembly should hold up across back-to-back shifts without drift, so operators aren't re-tuning at 2 a.m. That same stability translates into consistent coating thickness across large panels—no guessing whether the edges or center got the right deposit. Equally important is substrate flexibility. The best setups let you switch between different materials or part geometries without a full tooling overhaul, which saves hours of downtime and keeps small-batch runs viable.
Beyond the hardware, look for systems that treat process data as a live tool, not a log file. Real-time flow adjustments should be possible without halting the run, letting you correct minor deviations on the fly. Maintenance alerts need to surface before a fault shuts you down—think predictive warnings about nozzle wear or pump strain, not just error codes after the fact. And the data itself should be actionable mid-batch: trends in viscosity, flow rate, or coating thickness that help you tighten tolerances immediately rather than waiting for a post-run review. These capabilities separate a coating system that merely sprays from one that truly controls the outcome.
Contact Us
Contact Person: Ivy Zhang
Email: [email protected]
Tel/WhatsApp: +86 1081502288
Website: https://www.siansonic.com/